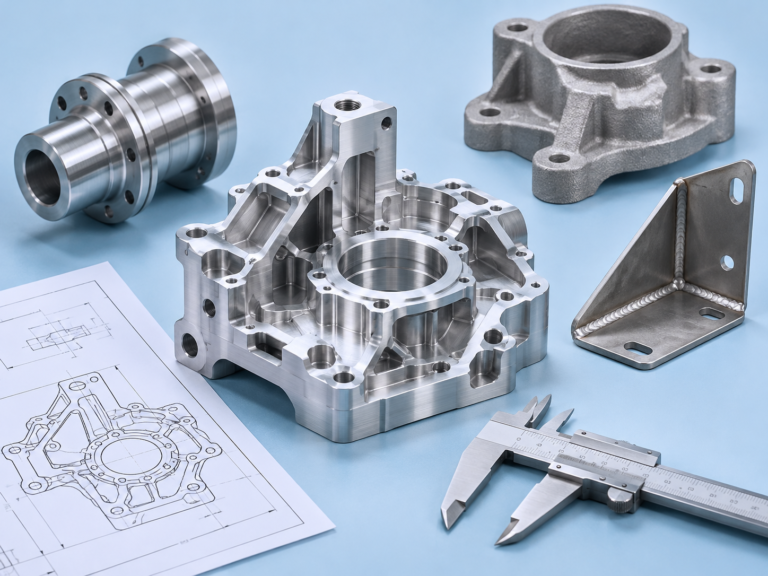
Casting vs CNC machining: how geometry, material, production volume, tooling costs, tolerances and finished-component requirements determine the better manufacturing method.
A component that costs €180 to manufacture from a solid metal block might cost considerably less when produced as a casting and finish-machined. But for another component, investing in casting tooling could make production more expensive rather than cheaper.
The difference often comes down to geometry, manufacturing quantity and how much material must be removed.
Casting becomes worth considering when the component has complex shapes, large internal cavities, significant material waste during machining or sufficient repeat demand to justify casting preparation and tooling. Machining from solid generally remains attractive when quantities are low, designs are changing frequently or the component is compact and requires extensive precision machining regardless of its starting form.
There is no universal production quantity at which casting becomes cheaper than CNC machining. A relatively simple component might never justify casting, while a large, hollow housing could make casting attractive at much smaller quantities.
The decision also involves more than price. Material properties, dimensional accuracy, production lead time, quality requirements and future design changes can determine whether switching processes is appropriate.
This article explains when casting is a better option, when machining from solid should remain the preferred method and how to compare both manufacturing routes without overlooking important costs.
Casting vs CNC Machining: What Is the Main Difference?
The fundamental difference is how the component obtains its shape.
CNC machining from solid starts with a bar, plate, billet or other stock material. Cutting tools remove unwanted material until the required geometry is achieved.
Metal casting starts with molten metal poured or introduced into a mould. After solidification, the casting is removed, cleaned and inspected. Critical surfaces may then be CNC-machined to their final dimensions.
Both methods can produce functional industrial components, but they distribute manufacturing effort differently.
Machining from solid generally requires less dedicated shaping tooling but potentially more material removal and machine time.
Casting may require patterns, moulds, process development and additional quality controls, but it can produce a shape much closer to the finished component.
Quick Comparison: Casting or Machining from Solid?
| Factor | CNC machining from solid | Casting followed by CNC machining |
|---|---|---|
| Initial tooling | Usually lower | Can require patterns, moulds or dedicated tooling |
| Design changes | Generally easier to implement | Can require tooling changes |
| Complex external shapes | May require extensive machining | Often attractive |
| Internal cavities | Limited by tool access and geometry | Can be produced using suitable cores or mould designs |
| Material waste | Potentially high | Often lower for complex shapes |
| Tight tolerances | Achievable directly with suitable processes | Critical features typically require finish machining |
| Small quantities | Often economical | Depends on casting process and tooling |
| Recurring production | Competitive for many geometries | Can become advantageous when machining savings justify preparation |
| Material properties | Based on selected wrought or stock material | Based on cast alloy, solidification and process controls |
| Quality risks | Machining defects, distortion, stock material issues | Porosity, shrinkage defects, inclusions and dimensional variation |
Neither process is automatically superior.
The best option is the one that meets the finished-component requirements at an acceptable total cost, risk and lead time.
1. When Large Amounts of Material Must Be Removed
One of the strongest reasons to investigate casting is excessive material removal.
Consider a housing produced from a rectangular steel or aluminium block.
The finished component may contain:
- A large central cavity.
- Several internal pockets.
- Mounting flanges.
- External ribs.
- Bearing locations.
- Thin connecting walls.
- Numerous holes and interfaces.
When manufacturing this component from solid material, a CNC machine may spend substantial time removing material that is not required in the finished part.
The raw block can also be significantly heavier than the final component.
That creates costs for material purchasing, rough machining, tool wear, coolant management, chip handling and machine occupancy.
Understanding Material Utilization
A useful initial indicator is the material utilization ratio:
Material utilization = Finished component mass ÷ Starting stock mass × 100%
Suppose a component is machined from a 30 kg aluminium block, but the finished part weighs only 8 kg.
Material utilization is approximately 27%.
This means approximately 73% of the starting material is removed during manufacturing.
The removed metal may have recycling or scrap value, but that does not recover the machining time, cutting-tool consumption or all the original material cost.
For a component with this geometry, casting could be worth evaluating.
A suitable casting may require considerably less rough machining because much of the required external shape and internal cavity structure is created during solidification.
However, casting also requires allowances for gates, risers, shrinkage, cleaning and subsequent machining. It is not a zero-waste process.
When Material Removal Is Not a Problem
Low material utilization does not automatically mean casting is cheaper.
A component may be inexpensive to machine when:
- The material is relatively easy to cut.
- High material-removal rates are possible.
- The part can be produced in few setups.
- The required quantity is small.
- Casting tooling would be expensive.
- The geometry is likely to change.
A meaningful comparison must include the actual cost of both finished production routes.
2. When the Component Has Complex Internal Cavities
Casting can be especially attractive for parts with internal geometries that are difficult or impossible to machine using conventional cutting tools.
Examples include:
- Pump housings with internal flow passages.
- Valve bodies.
- Gearbox casings.
- Fluid-handling components.
- Machinery housings with enclosed cavities.
- Components with complex hollow shapes.
Machining these features from a solid block may require specialized tooling, multiple setups or changes to the component design.
Some cavities cannot be reached by a conventional cutting tool at all.
How Casting Creates Internal Features
Certain casting methods use cores to produce internal voids.
During mould preparation, the core is positioned within the mould cavity.
Molten metal solidifies around the core, creating the desired internal passage or hollow region.
The core is subsequently removed using a process appropriate to the casting method.
This can make it possible to manufacture shapes that would be highly inefficient or inaccessible through ordinary CNC machining.
However, cores introduce their own manufacturing challenges.
Core placement, strength, removal, surface condition and dimensional variation must all be controlled.
Not every internal passage is suitable for every casting method.
Example: Industrial Pump Housing
A pump housing may require a complex flow passage together with highly accurate bearing seats and sealing interfaces.
Producing the entire housing from solid material could require substantial machining and may not be feasible as a single-piece design.
Casting can create the general housing geometry and internal flow passages.
CNC machining can then finish the critical functional features.
For such components, metal casting followed by CNC machining may provide a more suitable production route.
The critical requirement is ensuring that casting allowances, material properties, internal geometry and final machining requirements are considered together from the beginning.
3. When Production Quantities Justify Tooling Investment
Casting often involves higher preparation costs than machining from standard stock.
Depending on the method, these can include:
- Pattern design and manufacturing.
- Mould tooling.
- Core boxes.
- Casting process development.
- Initial samples.
- Tooling adjustments.
- First-article inspection.
- Casting qualification.
These investments may be difficult to justify for a small number of parts.
However, when the same component is produced repeatedly, the tooling cost can be distributed across a larger quantity.
How to Calculate the Break-Even Quantity
A simplified cost comparison is:
Total CNC cost = CNC preparation costs + Quantity × CNC unit cost
Total casting cost = Casting preparation costs + Quantity × Finished casting unit cost
The finished casting unit cost must include the cast blank, cleaning, inspection, relevant processing and all necessary CNC machining.
For a simple illustration, consider the following hypothetical quotations:
| Cost element | Machining from solid | Casting + CNC finishing |
|---|---|---|
| Initial preparation and tooling | €1,000 | €11,000 |
| Finished component unit cost | €125 | €85 |
| Unit cost difference | — | €40 lower with casting |
The casting route has €10,000 in additional initial costs but saves €40 per finished component.
The break-even quantity is therefore:
€10,000 ÷ €40 = 250 components
Under these assumptions, both processes have the same modeled total cost at 250 finished components.
At 500 components, the estimated totals are:
- CNC machining: €63,500.
- Casting with CNC finishing: €53,500.
- Estimated casting advantage: €10,000.
These are illustrative figures, not market quotations. They assume no changes in unit prices, yield, tooling maintenance, quality costs or other commercial conditions.
The real break-even point must be calculated using actual supplier quotations.
Why Annual Volume Alone Can Be Misleading
Imagine that a component has an estimated demand of 1,000 pieces per year.
At first glance, casting may seem attractive.
However, the decision also depends on whether the same geometry will remain in production.
If the component is expected to undergo major design changes after the first 100 pieces, tooling investment may become difficult to recover.
Conversely, a stable component required in smaller annual quantities over many years may justify tooling if the total lifecycle demand is sufficient.
The correct comparison should therefore consider the full expected production period, not simply the first purchase order.
4. When the Design Is Stable Enough for Casting
Design flexibility is one of the strongest arguments in favor of machining from solid.
For a component still undergoing development, dimensions and features may change frequently.
Machining from stock generally allows many changes to be implemented through revised CNC programs, tooling or fixturing.
Casting can be less flexible.
A change to the external geometry or internal cavity may require modifications to the pattern, mould or core tooling.
Some modifications may require entirely new tooling.
A Practical Product-Development Sequence
For certain industrial components, a sensible approach can be:
Prototype stage: Manufacture the component from solid material to validate fit, assembly and functionality.
Design validation: Confirm the geometry, operating requirements and critical tolerances.
Production planning: Compare machining from solid against casting followed by CNC finishing.
Casting qualification: Produce and inspect initial castings, verify required properties and establish the machining process.
Serial production: Release the approved casting-based production route.
This approach can reduce the risk of investing in casting tooling before the design is sufficiently mature.
However, there is an important limitation.
A prototype machined from wrought material is not necessarily mechanically equivalent to the same geometry produced as a casting.
Material behavior, defect populations, fatigue properties and manufacturing-induced stresses may differ.
Where these characteristics affect performance, the cast version must undergo appropriate engineering validation.
5. When Material Requirements Favor One Process
A common mistake is treating material selection as separate from manufacturing-process selection.
Cast and wrought materials are not automatically interchangeable.
A component machined from a rolled or forged alloy may have different mechanical behavior from a component produced using a cast alloy.
These differences may affect:
- Tensile and yield strength.
- Fatigue resistance.
- Impact properties.
- Ductility.
- Internal soundness.
- Corrosion behavior.
- Wear resistance.
- Performance under cyclic loading.
Cast Iron Components
Grey cast iron and ductile cast iron are widely used for industrial housings, machinery structures and other suitable components.
Grey cast iron can provide useful vibration-damping characteristics and good machinability in appropriate applications.
Ductile cast iron can offer a different balance of strength, ductility and casting characteristics.
The correct grade depends on the application’s mechanical and functional requirements.
Cast Steel Components
Cast steel may be suitable for structural or load-bearing components with geometries that benefit from casting.
However, casting defects, heat treatment, section thickness and material qualification can significantly affect finished-part performance.
A cast steel component should not automatically be treated as equivalent to one machined from wrought steel of a nominally similar composition.
Aluminium Castings
Aluminium casting can be attractive for complex lightweight housings and equipment components.
Different casting methods and alloys provide different mechanical properties and achievable geometries.
A casting alloy must be selected for the required production process and operating conditions.
If a component was originally designed using wrought aluminium such as 6061 or 7075, converting it to a cast aluminium alloy may require engineering review and validation.
Material substitution should never be based on manufacturing cost alone.
The new production route must satisfy the approved functional, mechanical and quality requirements.
6. When Tight Tolerances Are Required
It is sometimes assumed that casting is unsuitable for precision components.
That is not necessarily true.
A casting can serve as the starting form for a high-precision finished component.
However, casting alone generally does not provide the dimensional control required for every critical feature.
A practical approach is to cast the general shape and machine the precision interfaces afterward.
Which Features Typically Need CNC Finishing?
Examples include:
- Bearing bores.
- Sealing surfaces.
- Precision mounting faces.
- Threaded holes.
- Shaft interfaces.
- Dowel-pin locations.
- Critical hole patterns.
- Tight-tolerance diameters.
Other surfaces may remain as-cast when their surface condition and dimensional tolerances meet the design requirements.
This distinction is important because machining every surface of a casting unnecessarily can reduce the economic benefit.
Why Machining Allowances Matter
A cast blank must contain sufficient material on surfaces that require final machining.
The required allowance depends on factors such as casting method, dimensions, distortion, surface quality and process capability.
Too little allowance can result in incomplete cleanup or rejected finished parts.
Excessive allowance increases machining time and reduces some of the cost advantages of casting.
The machining plan should therefore be developed together with the casting design.
Datum Selection Is Equally Important
A casting may have greater dimensional variation than a machined stock blank.
The machining process needs reliable reference features to establish the final component geometry.
Critical relationships between bores, faces and mounting surfaces must be considered during fixture design and process planning.
For applications requiring tight final tolerances, CNC turning and milling services can be combined with casting to achieve the required precision on suitable features.
The finished component—not merely the rough casting—must satisfy the drawing.
7. When Casting Defects and Quality Risks Become Important
Casting can reduce machining effort, but it introduces manufacturing risks that differ from those of machining wrought stock.
Possible casting-related defects include:
- Gas porosity.
- Shrinkage cavities.
- Inclusions.
- Cold shuts or incomplete fusion.
- Incomplete mould filling.
- Dimensional distortion.
- Surface discontinuities.
- Internal defects exposed during machining.
The relevance and acceptability of these defects depend on the component’s function and the agreed inspection requirements.
For example, a small surface imperfection may be acceptable on a noncritical exterior region but unacceptable on a sealing face or pressure-retaining wall.
Why Some Defects Appear Only After Machining
A rough casting may look acceptable before CNC machining.
However, material removal can expose internal porosity or shrinkage defects.
This becomes particularly problematic when a defect appears in a precision bore, sealing surface or another functional region.
At that stage, substantial manufacturing value may already have been added to the component.
This is why the casting and machining operations should not be planned independently.
What Should a Casting Quality Plan Include?
Depending on the component, a suitable quality plan may cover:
- Material grade and certificate requirements.
- Chemical composition and mechanical properties.
- Dimensional inspection of castings.
- Visual inspection.
- Non-destructive testing where appropriate.
- Pressure or leak testing when required.
- Machining allowance verification.
- Inspection after final CNC machining.
- Traceability between casting batches and finished components.
Non-destructive testing methods may include radiographic, ultrasonic, magnetic-particle or liquid-penetrant examination, depending on the material, geometry and inspection objective.
The acceptance criteria should be defined before production.
A supplier should not simply promise that a casting will be free of every microscopic discontinuity without a realistic and measurable specification.
8. Choosing Between Sand Casting, Investment Casting and Die Casting
The term “casting” covers several manufacturing methods with very different cost structures and capabilities.
Selecting the correct casting process is as important as deciding whether casting is suitable at all.
Sand Casting
Sand casting is frequently considered for larger or more complex metal components, including industrial housings and machine structures.
It can accommodate various ferrous and non-ferrous alloys and can be suitable for low-to-medium quantities, depending on tooling and component requirements.
Typical applications include:
- Pump housings.
- Gearbox casings.
- Machine bases.
- Large industrial brackets.
- Cast iron equipment components.
Sand casting may require significant finishing on precision surfaces.
Investment Casting
Investment casting, sometimes called lost-wax casting, can be attractive for smaller or medium-sized components with complex shapes and detailed features.
It can reduce certain machining requirements compared with rougher casting methods.
However, tooling, component size, alloy requirements and inspection needs influence feasibility and cost.
It may be appropriate for selected stainless steel, steel and other alloy components.
Die Casting
Die casting can be an efficient method for suitable alloys and geometries, particularly at higher production volumes.
It often offers productive manufacturing cycles and relatively consistent geometry.
However, dedicated tooling can be expensive, and alloy, process, size and design constraints must be considered.
Not every metal alloy or industrial component is suitable for conventional pressure die casting.
Comparison of Casting Methods
| Method | Often attractive for | Main consideration |
|---|---|---|
| Sand casting | Large housings, iron and steel components, selected small and recurring batches | Surface finish, dimensional variation, process control |
| Investment casting | Detailed geometries and selected precision components | Tooling, size limits, process economics |
| Die casting | Suitable high-volume aluminium and other non-ferrous components | Higher tooling investment and process constraints |
MegaMETA supports sand casting, investment casting and die casting through its manufacturing network, including subsequent machining where required.
The appropriate method should be selected after reviewing the part geometry, material, quantity and final acceptance requirements.
9. When Casting Can Increase Costs Instead of Reducing Them
Casting is not always the cheaper solution, even for a complex component.
Several factors can make casting uneconomical.
Frequent Drawing Revisions
If the component’s shape changes repeatedly, tooling modification costs may outweigh machining savings.
Very Small Quantities
A one-off component may be cheaper to machine from stock even if material utilization is poor.
The same can apply to small batches, although simpler casting methods may remain feasible in certain cases.
Extensive Final Machining
If most surfaces require precision machining, casting may save less machining time than expected.
The cost benefit depends on which operations are actually eliminated or shortened.
Difficult Casting Geometry
Certain geometries create mould-filling, solidification, core-removal or defect-control problems.
A component that appears well suited to casting based on its external shape may require substantial design changes.
High Rejection Rates
Low casting yield, dimensional variation or defects discovered during machining can increase the cost of acceptable finished parts.
Material Restrictions
The originally specified material may not have a suitable casting equivalent that meets the component’s functional requirements.
Long Tooling Lead Times
If a component is required urgently, a casting route involving new tooling and sample qualification may not meet the necessary schedule.
The correct decision is based on the cost and reliability of accepted finished components, not simply the purchase price of a rough casting.
10. Compare the Total Cost of a Finished Component
When comparing casting and machining from solid, it is important to request equivalent quotations.
One quotation may include only a rough casting.
Another may include a fully machined component with surface treatment, inspection and delivery.
These offers cannot be compared directly.
A proper cost comparison should consider:
| Cost element | Machining from solid | Casting + machining |
|---|---|---|
| Raw material or blank | Bar, plate or billet | Cast component |
| Dedicated tooling | Fixtures and selected tools | Patterns, moulds, cores and machining fixtures |
| Programming and setup | CNC operations | Casting preparation and CNC operations |
| Machining | Complete geometry | Critical and required surfaces |
| Heat treatment | As specified | As specified and compatible with cast material |
| Inspection | Material and finished-part verification | Casting inspection plus finished-part verification |
| Scrap and rework | Machining-related losses | Casting and machining-related losses |
| Transport | Material and finished parts | Potential movement between foundry and machining facility |
| Tooling maintenance | As applicable | As applicable |
| Delivery | Finished component | Finished component |
The Importance of Accepted-Part Cost
Suppose a casting supplier quotes €50 for each rough casting, and the finishing operation costs €30.
The apparent finished cost is €80.
But if some castings fail inspection or are rejected during machining, the effective cost per acceptable component increases.
For example, if a process incurs €8,400 in recurring production costs for 100 attempted components but produces only 95 accepted finished parts, the effective recurring cost is approximately €88.42 per accepted part.
This simplified example excludes tooling and other lifecycle costs, but illustrates why scrap and quality performance matter.
A comparable assessment should also consider scrap and rework in the machining-from-solid route.
The purchasing decision should use realistic process yields for both alternatives.
11. How to Evaluate Switching an Existing CNC Part to Casting
Switching a component that is already being machined from solid requires more than obtaining a casting quotation.
The new manufacturing process may influence dimensions, material behavior, inspection and approval requirements.
A structured transition reduces the risk of replacing an established process with one that is cheaper on paper but problematic in production.
Step 1: Review the Current Manufacturing Cost
Understand where the current unit cost comes from.
Is the main expense raw material, rough machining, finishing, workholding or inspection?
If material removal is not a major cost driver, casting may provide little financial benefit.
Step 2: Confirm the Expected Production Demand
Consider initial orders, annual quantities, future demand and expected product lifetime.
Avoid making tooling decisions solely on an optimistic forecast.
Step 3: Assess Casting Feasibility
Evaluate the selected alloy, wall thickness, geometry, cavities, draft, cores and solidification requirements.
Determine whether the component can be cast without compromising essential functional requirements.
Step 4: Identify the Necessary CNC Operations
Establish which surfaces require machining and how the casting will be located during those operations.
Include appropriate allowances and inspection requirements.
Step 5: Calculate the Full Cost
Compare tooling, recurring production cost, scrap, inspection, logistics and expected future revisions.
Calculate the break-even quantity using actual quotations.
Step 6: Produce and Validate Samples
Inspect initial castings and finished machined components.
Where relevant, validate mechanical properties, pressure integrity, fatigue behavior, assembly fit and functional performance.
Step 7: Approve the Production Change
The responsible design authority should approve any required material, drawing or process changes.
For controlled production components, formal validation or customer approval may be required.
Step 8: Release Repeat Production
Once the casting route is validated, establish production documentation, quality controls, tooling arrangements and recurring delivery expectations.
Do not discontinue the existing manufacturing route until the replacement has been appropriately qualified and the transition risk is acceptable.
12. Practical Examples: Which Method Is Better?
The following examples are illustrative. The best route for an actual component depends on its drawing, material, quantity and functional requirements.
Example A: Aluminium Housing with Several Internal Pockets
Component: Aluminium equipment housing.
Quantity: 800 pieces annually.
Challenges: Large material removal volume and multiple internal features.
Potential choice: Casting followed by CNC machining.
Reason: A form-near-net casting could reduce material removal and machining time, provided an appropriate casting alloy can satisfy the engineering requirements.
Example B: Stainless Steel Precision Block
Component: Compact stainless steel block with precision bores and mounting holes.
Quantity: 15 pieces.
Challenges: Tight tolerances but relatively straightforward geometry.
Potential choice: CNC machining from solid.
Reason: Casting preparation would likely add complexity, while the component can be machined using accessible features and existing stock material.
Example C: Large Cast Iron Machine Base
Component: Machine base with ribs, cavities and precision mounting interfaces.
Quantity: 60 pieces annually.
Challenges: Large overall dimensions and complex geometry.
Potential choice: Sand casting followed by machining.
Reason: Casting may provide a practical way to produce the bulk shape while CNC machining establishes accurate mounting surfaces.
The choice depends on tooling economics, design maturity and suitable casting quality.
Example D: Prototype Valve Body Under Development
Component: Valve body with several internal passages.
Quantity: Five prototypes.
Challenges: Frequent design changes and functional validation.
Potential choice: CNC machining or another prototype manufacturing route.
Reason: The flexibility of machining may outweigh the potential long-term benefits of casting.
If the component later enters recurring production, casting can be reassessed.
Example E: High-Volume Aluminium Transmission Housing
Component: Housing with relatively stable geometry and precision bearing locations.
Quantity: Several thousand pieces per year.
Challenges: Repeated production, high material removal and tight final machining requirements.
Potential choice: A suitable casting process combined with CNC finishing.
Reason: Higher production volume may support tooling investment, while casting can reduce the amount of material removed during each cycle.
The manufacturing method still depends on alloy requirements, casting feasibility, inspection and total production economics.
13. What Information Is Needed to Compare Casting and CNC Machining?
A useful quotation comparison requires more than a 3D model and the requested quantity.
The following information makes it easier to evaluate both production routes.
| Required information | Why it matters |
|---|---|
| 2D technical drawing | Defines dimensional and acceptance requirements |
| 3D CAD model | Supports geometry and manufacturing feasibility review |
| Material and standard | Determines material and process compatibility |
| Initial quantity | Supports quotation of the first order |
| Annual quantity | Helps assess tooling investment |
| Expected production lifetime | Supports lifecycle cost analysis |
| Critical tolerances | Identifies required precision finishing |
| Functional requirements | Helps evaluate alternative materials and processes |
| Heat treatment | Influences properties and manufacturing sequence |
| Surface treatment | Affects dimensions, finishing and cost |
| Quality documentation | Defines inspection and traceability requirements |
| Current production method | Provides a baseline for comparison |
| Current cost or target cost | Helps identify whether a change is worthwhile |
| Delivery requirements | Defines commercial and scheduling constraints |
When a component is already in serial production, the current method’s material consumption, cycle time and rejection history can be especially valuable.
Where confidential cost information cannot be shared, a target price or a description of the main cost problem may still help guide the evaluation.
Request Two Separate Manufacturing Quotations
For an appropriate component, ask for:
Option A: CNC machining from solid material.
Include all operations necessary to deliver the finished component.
Option B: Casting followed by CNC machining.
Include pattern or tooling costs, casting, cleaning, finishing, final machining, inspection and documentation.
For both options, request prices at relevant quantities and distinguish one-time charges from recurring costs.
The result should be a comparison of finished, acceptable components produced to the agreed specification.
14. Combining Casting and CNC Machining Through One Manufacturing Partner
When the casting and CNC machining operations are managed by separate suppliers, the purchasing process may become more complicated.
A rough casting must arrive with appropriate dimensions, sufficient machining allowance and acceptable quality.
The machining supplier must then establish accurate reference features and finish the component.
If problems occur, determining responsibility can be difficult.
For example, a casting may have inadequate machining stock on a critical surface.
The issue may become visible only when the machining operation starts.
If the foundry and machining supplier have not agreed on the required allowances and reference features, the result can be rework, delays or rejected components.
Why Coordination Matters
A coordinated production route can establish responsibility for:
- Casting design and manufacturability.
- Pattern and tooling requirements.
- Material specifications.
- Machining allowances.
- Casting inspection.
- CNC process planning.
- Final dimensional inspection.
- Quality documentation.
- Delivery of finished components.
MegaMETA coordinates metal casting services and CNC machining services through its European manufacturing partner network.
This allows casting and machining requirements to be reviewed as connected production stages rather than independent purchasing decisions.
The suitability of each process and the complete project scope are evaluated according to the component’s technical requirements.
Frequently Asked Questions About Casting vs CNC Machining
Is casting cheaper than CNC machining?
Casting can be cheaper when complex geometry, material waste or recurring production volumes justify the initial casting preparation costs. CNC machining may remain more economical for low quantities, simple geometries or frequently changing designs.
At what production quantity does casting become cheaper?
There is no universal break-even quantity. The result depends on tooling investment, unit manufacturing costs, geometry, material, finishing requirements and expected scrap. Actual supplier quotations are needed to calculate the break-even point.
Can cast parts achieve tight tolerances?
Yes, when suitable castings are followed by precision CNC machining or other appropriate finishing processes. Critical bores, mounting faces and sealing surfaces are commonly machined after casting.
Is casting suitable for prototypes?
It can be, depending on the casting method, part size and tooling requirements. However, machining from solid may be more flexible for prototypes that require frequent design modifications.
Can a part originally machined from steel be converted to a steel casting?
Potentially, but the material and manufacturing change must be assessed. Cast and wrought steel components may have different mechanical properties and defect characteristics. Engineering validation may be necessary.
Why are gearbox housings often cast?
Casting can efficiently produce housings with ribs, cavities and complex outer geometries. Critical bearing seats, bores and mounting faces can then be CNC-machined to the specified dimensions.
Does casting eliminate CNC machining?
Not necessarily. Many cast components still require precision machining of functional surfaces, holes and interfaces. Casting primarily reduces the need to machine the overall bulk geometry from solid stock.
Which casting method is best for industrial components?
The appropriate method depends on the material, geometry, size, quantity and quality requirements. Sand casting, investment casting and die casting offer different capabilities and economic advantages.
What risks should be considered when switching from machining to casting?
Important risks include tooling investment, dimensional variation, casting defects, material-property differences, machining allowances, production lead time and the need to requalify the finished component.
Can MegaMETA supply fully machined cast components?
MegaMETA coordinates casting and subsequent CNC machining through its manufacturing network. Projects can include casting, finishing, machining and agreed inspection requirements, subject to technical feasibility.
Conclusion: When Does Casting Make More Sense Than Machining from Solid?
Casting is worth investigating when a component requires substantial material removal, contains complex internal cavities or has recurring production demand that can justify tooling investment.
Machining from solid generally remains attractive for prototypes, small quantities, changing designs and components whose geometry can be produced efficiently through conventional machining.
The decision should not be based on production quantity alone.
Material properties, final tolerances, casting quality, tooling costs, machining requirements and expected product lifetime all influence the outcome.
For many industrial components, the most effective solution is not choosing casting instead of CNC machining.
It is combining casting and CNC machining so that each process performs the operations it handles most efficiently.
Considering Casting Instead of Machining from Solid?
If your current component requires extensive machining, produces excessive material waste or has become expensive at higher production volumes, MegaMETA can evaluate whether a casting-based manufacturing route is technically and economically appropriate.
Send your technical drawings, CAD models, material requirements, quantities and critical specifications for review.
MegaMETA can assess suitable casting processes, required CNC finishing operations and the feasibility of supplying a complete finished component.
Explore MegaMETA Casting Services
Explore MegaMETA CNC Machining Services
Request a manufacturing quotation through MegaMETA to compare suitable production alternatives for your component.